
Ordering Custom Forged Ball Valves? Confirm These Details Before Production Starts ? | drawing approval, marking request, inspection scope
Drawing size tolerance (±0.05mm), material standard (such as ASTM A105), pressure class (Class 150–2500), marking content and position (marking depth 0.3mm), inspection scope (100% water pressure + 10% spot check RT), and sign drawing and inspection plan after then can put into production. drawing approval Size & Flange Connection ASME B16.10 specification divides long and short series very clearly. On a 2-inch 150-pound drawing if it writes 178 millimeters, it shows it is short series, if writes 216 millimeters then is long series. This 38 millimeters drop, will let site workers take welding torch to cut off pipe and re-grind. 10 inches and below sizes, end to end length error is strictly limited within plus or minus 1.6 millimeters. In large petrochemical pipe galleries, once flange appears 2 millimeters deviation, forcefully pulling to butt joint will let connection bolts bear extremely large shear stress. Drawing approval confirms tolerance column writes clearly plus or minus 1.6 millimeters, site assembly then will not get stuck. Consult ASME B16.5 specification, flange outer diameter, bolt hole center circle diameter and hole opening quantity are all one to one bound. 2-inch 150-pound flange outer diameter is 150 millimeters, above opens 4 pieces of 19 millimeters bolt holes. Pound class increases to 300 pounds, outer diameter will expand to 165 millimeters, hole quantity also doubles to become 8 pieces. Hole opening diameter on drawing wrongly marks one millimeter, site M16 studs then cannot pass into flange. On drawing these several flange details often are wrongly marked: Flange total thickness misses calculating raised face height value Bolt holes not according to straddle centerlines principle to carry out array Blind hole thread depth shorter than 1.5 times inner hole diameter Ring groove bottom chamfer fillet radius turned too small On 150-pound and 300-pound drawings, this step nominal height is specified as 2 millimeters. When pipeline pressure reaches 400 pounds and above, height marking on drawing must become 7 millimeters. These few millimeters metal protrusion, controls two pieces flange between spiral wound gasket’s compression rebound amount. On drawing must detailedly write out trapezoidal ring groove’s pitch diameter, groove width and groove depth’s specific numbers. 900-pound flange octagonal gasket ring groove angle is fixed dead at 23 degrees, processing tolerance only allows deviating 0.5 degrees. Factory lathe tool deviates 0.5 degrees, metal seal ring puts inside then will happen line contact leaking gas. Line of sight passes through flange to enter valve body inner cavity, channel inner diameter size interferes with fluid passing pressure drop. Ordinary drawing will fuzzily mark a DN50, full bore ball valve according to API 6D requirement, inner hole diameter actual measurement needs to reach 49 millimeters above. Inner hole number on drawing if is secretly reduced to 38 millimeters, pig forcefully entering pipeline bound to will get stuck dead in the middle of ball. ASME B16.34 standard table 3 gives wall thickness drawn a red line. 4-inch 600-pound forged steel valve body, minimum wall thickness is not allowed thinner than 11.1 millimeters. On drawing if only casually marks a 10 millimeters, high pressure fluid produces water hammer impact time, valve body weak zone very easily tears open tiny cracks. On these several internal sizes, manufacturers extremely easily compress metal materials: Valve seat seal ring radial thickness allowance Anti-blowout valve stem step width width Between ball upper part and valve cover metal clearance value Flange neck transition fillet radius size NPT thread marking will attach a taper data, industry convention is 1 to 16. According to ASME B1.20.1 specification, 2-inch NPT outer thread reference plane effective length is fixed at 17.32 millimeters. Butt welding end wall thickness exceeds 22 millimeters time, drawing must draw out compound type U-V groove shape cross section. Partial enlarged drawing inside has a string of models complying with ISO 5211 specification. Marking F07, four bolt holes distribution circle diameter then is fixed at 70 millimeters, drills out 4 pieces of M8 thread holes. Valve stem square head opposite side size marks 14 millimeters or 17 millimeters, with gear box inner hole implements H9 and d11 clearance fit. Unmarked tolerance sizes approval extremely tests mechanical processing common sense. Technical column often prints has “unmarked linear sizes according to GB/T 1804-m level execute” words. On drawing a marked as 100 millimeters outer shape non-fit length, actual object turning will between 99.7 millimeters to 100.3 millimeters float. BS 6364 standard writes, pipeline temperature low to minus 100 degrees Celsius time, in order to prevent packing freeze hard lose elasticity, gas chamber length must be greater than 250 millimeters. On drawing lacks this long neck’s specific height data, site cooling freezing cold bridge will all the way spread to operation handle. An 8-inch 1500-pound forged steel ball valve actual weight approaches 850 kilograms. This number controls site crane driver’s lifting weight model selection and pipeline support’s load-bearing estimation. Shipped to site actual object weight if compared to drawing less fifteen percent, factory mostly is cut valve body outer wall’s turning metal allowance. Pipe network system’s safety redundancy, disperses in drawing various parts’ hidden parameters inside: Valve cover double-head studs’ tensile yield strength value Pressure-bearing boundary minimum thickness tolerance’s lower limit value Operation gear box nameplate on maximum torque value Actuator cylinder’s working air pressure lower limit value On drawing will draw out valve stem inside stuffed a tiny spring and metal steel ball. Spring’s free length is marked as 8 millimeters, compression amount is conventionally set at 2.5 millimeters. Spring force not in place, ball friction produced static electricity cannot be conducted to valve body, potential breaks through 300 volts extremely easily in natural gas pipeline inside causes electric sparks. Material & Parameters ASTM A105N is carbon steel forgings’ frequent customer, that “N” represents normalizing heat treatment. After 1.5 hours’ 880°C to 920°C normalizing, metal grains get refined, ensure under minus 29°C environment, impact work value still can keep at 27 Joules above. If pipeline transported medium contains hydrogen sulfide, drawing must forcibly mark complies with NACE MR0175 standard. Valve body and internal parts’
Soft Seated or Metal Seated Forged Ball Valve: Which Option Fits Your Application | sealing method, media condition, temperature range
Soft seated ball valves are suitable for clean media, temperature ≤200°C, leakage class can reach ANSI Class VI; metal seated are suitable for particle-containing or high-temperature conditions (≤550°C), erosion resistant but leakage class is generally Class IV. Selection should be based on media particle content, temperature range, and opening/closing frequency, and combined with sealing surface hardening treatment (such as HVOF spraying) to improve lifespan. sealing method Soft Seated Polytetrafluoroethylene (PTFE) crystal melting point is 327 degrees Celsius, molecular weight is usually between 500,000 to 5,000,000. This polymer material exhibits physical stability in the range of minus 196 degrees Celsius to 200 degrees Celsius. Its friction coefficient is extremely low, with a value of only 0.04 in a dry friction state. When choosing PTFE for forged steel ball valve seats, the material density needs to be maintained between 2.14 g/cm3 to 2.20 g/cm3. Its tensile strength should reach around 28 MPa. When the fluid media pressure rises above 2.0 MPa, pure PTFE is prone to cold flow phenomenon, leading to changes in the sealing shape. In order to reduce deformation caused by cold flow, 15% or 25% glass fiber is added to polytetrafluoroethylene to make reinforced polytetrafluoroethylene (RPTFE). The linear expansion coefficient of this modified material drops to 6 times 10 to the power of negative 5 per Kelvin. In an environment of 150 degrees Celsius, its compressive strength is doubled compared to pure PTFE. PTFE (Polytetrafluoroethylene): density 2.16 g/cm3, water absorption rate lower than 0.01%, resistant to strong acids and alkalis. RPTFE (Reinforced Polytetrafluoroethylene): glass fiber ratio 15%, pressure bearing capacity supports Class 300 level. PEEK (Polyetheretherketone): melting point 343 degrees Celsius, hardness above Shore D 85, adapted to high pressures above Class 1500. Devlon V-API: water absorption rate is extremely low, only 0.08% at 20 degrees Celsius, mostly used for long-distance natural gas pipelines. Nylon 12 (Nylon): higher toughness, working temperature range is minus 40 degrees Celsius to 120 degrees Celsius. In high pressure environments, PEEK material demonstrates excellent mechanical support. This semi-crystalline polymer can still maintain a tensile modulus of about 1.0 GPa at 250 degrees Celsius. Its radiation resistance dose can reach 1100 Mrad. In severe conditions such as oil drilling and production, PEEK valve seats can withstand a pressure difference of 70 MPa without fracturing. After material properties are determined, they must be matched through processing accuracy. Usually, the roundness tolerance of a 4-inch ball should be limited to within 0.0127 mm. The ball surface roughness needs to reach between Ra 0.1 micron to Ra 0.2 micron. The specific pressure generated by valve seat pre-tightening must be higher than the media pressure. If the media pressure is 10 MPa, the specific pressure on the valve seat sealing surface should be set between 15 MPa to 22 MPa. Excessively high pressure will cause the operating torque to rise significantly, affecting the lifespan of the actuator. When calculating torque, the friction force between the ball and the valve seat must be included. Friction torque accounts for more than 60% of the total torque. For DN100 specification ball valves, under a 2.5 MPa pressure difference, the opening torque of the PTFE valve seat is approximately 120 Nm. When designing the matching actuator, a safety factor of 1.5 times is usually reserved. Ball roundness: 0.01 mm to 0.03 mm, ensuring uniform force on the contact surface. Surface hardness: the ball surface is usually plated with hard chrome, thickness 0.03 mm to 0.05 mm, hardness reaches HRC 55. Fitting clearance: the interference fit between the valve seat and the ball is usually set at 0.3 mm to 0.8 mm. Automatic pressure relief: when the valve cavity pressure exceeds the downstream pressure by 1.1 times, the valve seat should be able to automatically push open to relieve pressure. API 607 fire safety standard requires soft seated ball valves to still possess sealing capability after a fire occurs. In a fire, soft seats will quickly decompose and disappear above 400 degrees Celsius. At this time, the metal edge on the valve seat bracket must fit tightly with the ball to form a secondary metal seal, preventing large-scale media ejection. API 6D specification has strict quantification for leakage amount. Soft seated valves must reach ISO 5208 Class A standard, which means in a continuous 2-minute pressure test, the number of bubble leaks is zero. Tests usually use dry air or nitrogen. The test pressure is set at 1.1 times the maximum rated working pressure. Molecular structure determines the service life of the seal. The C-F bond energy in the PTFE molecule is extremely high, reaching 485 kJ/mol. This stable molecular chain allows the material to not easily undergo natural aging over an operating cycle of more than 10 years. When the flow velocity exceeds 5 meters per second, tiny impurities carried by the fluid will produce an erosion effect. If the hardness of impurities exceeds Shore D 60, it will leave permanent scratches on the soft seat surface. For high flow velocity conditions, an anti-erosion ring made of stainless steel is usually added to the front of the valve seat. Sealing lifespan: can reach 20,000 to 50,000 opening and closing cycles in a laboratory environment. Cleaning requirements: degreasing treatment is required before assembly to ensure no particles above 0.1 mm remain. Temperature rise speed: the heating rate should be controlled within 10 degrees Celsius per minute to prevent the generation of thermal stress cracks. The thermal expansion rate of polymers is 10 times higher than that of stainless steel. When the temperature rises from 20 degrees Celsius to 150 degrees Celsius, valve seat volume expansion will cause the torque to increase by more than 30%. Sufficient space must be reserved in the design to compensate for thermal expansion and contraction. 2 to 4 pieces of disc springs are often installed on the back of the valve seat to provide continuous thrust. Compared to casting parts, forged steel has better fatigue strength under 40 MPa high pressure. 17-4PH stainless steel is mostly used for
API Forged Ball Valve Buying Guide for Distributors and EPC Contractors | API compliance, project demand, supply stability
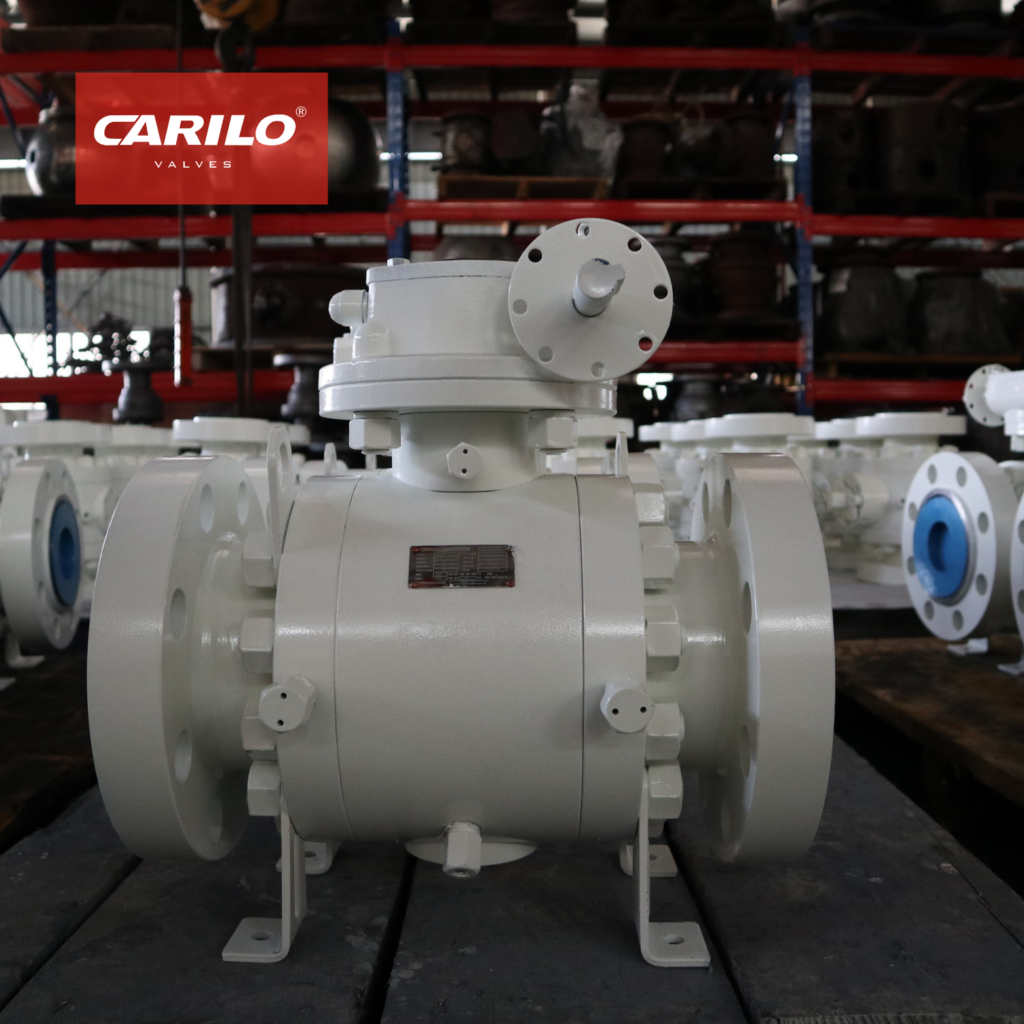
API forged ball valve selection needs to satisfy API 6D standard (covering 150–2500 pressure levels), and provide MTC, pressure test reports and other complete documents; Preferably select manufacturers with API licenses (such as 6D certification number), ensuring 100% hydrostatic and air-tightness testing. EPC projects suggest locking delivery time ≤8 weeks, stock rate ≥30%, and adopting DBB structure to improve sealing reliability. API compliance API Standard Code Take out a digital display vernier caliper and compare it with the API 608 standard manual, you will find its wall thickness requirement is about 3 mm more than ASME B16.34. These extra few millimeters of metal are not to add weight, but to allow the valve to withstand more than 10,000 mechanical cycles without generating metal fatigue during the dozens of frequent openings and closings every day in a refinery. A 12-inch Class 900 ball valve, the flow path inner diameter must solidly reach 305 mm. Some non-standard products, to save material, reduce the ball bore to 280 mm; this 25 mm difference will cause the pipeline pig to instantly get stuck when passing through, causing physical paralysis of the entire pipeline section. When engineers check API 6D drawings, their eyes will sweep toward the thrust shoulder at the bottom of the valve stem. This thickness is usually stuck between 5 mm to 10 mm; it is the last physical barrier to prevent the valve stem from becoming a “bullet” flying out under 150 bar high pressure. Even if the external gland bolts are all rusted off, this shoulder will deathly hold against the internal pressure. API 6D has clear hard indicators for physical parameters: Ball valves above 8 inches must be equipped with support feet or lifting lugs, with a load-bearing capacity not less than 2 times the total weight of the valve. The travel allowance of the seat ring needs to be reserved at 1.5 mm to 3 mm, ensuring automatic compensation after seal wear. The resistance value of the valve stem anti-static spring must be stable below 10 ohms, preventing accumulated charges from igniting the medium in the pipe. The flow path drop of full-bore valves must not exceed 0.5 mm, ensuring that the fluid will not produce eddy current erosion when passing through. Flipping through the API 607 fire test records, those are survival data burned out by real fire. The test requires the valve to be continuously burned in a flame of 750 degrees Celsius for 30 minutes. At this temperature, the PTFE sealing ring has already turned to ash. API 6FA is mainly prepared for those large-diameter valves on long-distance oil and gas pipelines. It requires higher pressure holding, usually reaching more than 75% of the rated working pressure. Under such extreme high temperatures, the thermal expansion of an 18-inch valve body will exceed 5 mm; the valve seat must have enough floating space to digest this deformation. The data density in the material report determines the survival rate of the valve in a hydrogen sulfide environment. When implementing the NACE MR0175 standard, the hardness of internal parts for API 6D valves is forcibly suppressed: The Rockwell hardness (HRC) of the valve stem and ball must not exceed 22 at maximum. The nickel content of carbon steel materials is strictly limited to below 1.0%, preventing hydrogen-induced cracking from occurring. The forging ratio must reach 4 to 1, ensuring the metal fiber flow direction is completely consistent with the force direction. Each batch of forgings must undergo 100% hardness sampling inspection, with the deviation value controlled within HB 10. Looking at the pressure test bench of API 598, every tick of the pointer jump relates to the safety of on-site workers. For a Class 1500 high-pressure ball valve, the hydrostatic shell test pressure will be directly hit to 38.2 MPa. Maintaining for 5 minutes at this pressure, even if the valve body surface oozes a layer of mist-like sweat, this valve belongs to scrap. The range of the pressure gauge should be selected between 1.5 times to 4 times the test pressure to ensure reading accuracy. The air-tightness test on the test bench uses 0.6 MPa of clean compressed air. The operator immerses the valve into a transparent water tank and holds breath to observe for 300 seconds. API 598 stipulates that as long as a bubble with a diameter exceeding 1 mm pops up on the water surface, the sealing performance is judged as unqualified. The pressure-temperature curve chart in ASME B16.34 is a life-and-death map. A WCB carbon steel valve can hold 51.1 bar at 38 degrees Celsius, but when the pipeline temperature rises to 425 degrees Celsius, its pressure-bearing capacity will drop off a cliff to 5.5 bar. If the purchaser only looks at the pressure rating at room temperature and ignores the reduction factor at high temperature, the valve will be stretched and deformed like plasticine at the site. In coastal high salt spray environments, the dry film thickness (DFT) should be applied in three layers, with a total thickness of not less than 250 microns. The zinc powder content of the first layer of zinc-rich primer must exceed 80%; this is using the primary battery principle to put a layer of chemical protective clothing on the iron lump, and the anti-corrosion life should match the 20-year design cycle of the project. Cost & Compliance The ex-factory price of a 2-inch Class 600 A105 forged steel ball valve ranges from 350 yuan to 900 yuan. In this 550 yuan price difference, hides the raw material traceability cost under the API Q1 system. The unit price per ton of round steel purchased by regular large factories is more than 15% more expensive than “low-quality scrap steel” without traceability documents. If a distributor, to save this 15% cost, goes to purchase unlicensed valves, the goods will hit the first wall upon arriving at the port. The EN 10204 3.1 certificate required by international engineering must be stamped by the factory laboratory and accompanied by a
What Makes a Reliable Forged Ball Valve Manufacturer for Export Business | export experience, quality control, international approval
Reliable forged steel ball valve export factory look at three points: ① export experience ≥ 5 years, annual shipment ≥ 5000 units; ② Quality control: need API6D/ISO9001, 100% shell pressure test + sampling inspection 10%; ③ Certification: CE, ATEX complete. Suggest on-site inspecting factory and sampling re-inspecting. export experience Technology & Specification Taking two inches size’s 800 pounds level forged steel ball valve to say, American engineer formulated’s wall thickness bottom line is 6.4 millimeters. Workshop master uses vernier caliper to measure size, hand slightly one shakes differed 0.02 millimeters, pipe inside’s 13.8 megapascals’ pressure then will take this layer iron skin prop broken. A piece carbon steel put on forging press bench on, furnace fire temperature from 1200 degrees Celsius slowly drops to 800 degrees Celsius. In order to find out these hiding at dark place’s tiny flaws, ultrasonic flaw detector’s probe needs to stick to iron lump surface slide one circle, 0.5 millimeters big’s sand hole immediately shows original shape. Foreign buyer hand inside got’s that copy English material sheet on, explicitly marked carbon element cannot exceed 0.25%. Factory inside’s machine forcefully pulls little steel strip, until pulled broken’s that one instant, tested out can carry 250 megapascals above’s strength, this batch iron material then has qualification to be sent onto lathe to cut. Carbon content indicator controlled at 0.43 inside Minus 46 degrees can resist 27 Joules impact Surface hardness maintained at 137 to 187 between Steel stamp striking depth fixed at 0.8 millimeters Ordinary plastic gasket if encounters 150 degrees Celsius’s boiling hot liquid, immediately then will soften into a puddle mud. Changed to special macromolecule PEEK material, bluntly can take carry burning’s bottom line pull high to 260 degrees Celsius. Fire again bigger a little even special plastic all cannot prop up, worker must change on pure metal’s sealing ring. Mechanical arm will at ball body outside evenly spray on a layer tungsten carbide, sprayed out’s this layer film thickness exactly stuck at 0.3 millimeters. Sprayed on this layer film after, surface hardness directly surges to 1200 Vickers hardness. Two iron parts face on coated full diamond abrasive paste, mutually back and forth rub on tens of thousands times, until surface like mirror same smooth, roughness low to 0.4 micrometers. Put into water tank inside doing holding breath test, 5 minutes inside water surface if emits out a mung bean big’s bubble, this batch goods then must all return re-do. Worker needs to at valve gap inside deadly stuff into 5 circles high purity graphite ring, using torque wrench uses out 30 Newton meters’ strength taking screw thoroughly twisted dead. Helium mass spectrometer that root needle same thin’s probe, sticking metal root part little by little moving, fully needs to smell on 15 seconds then considered checked finished. Screen on jumped out’s leaking air number, must compared to 10’s negative 5 power even smaller then considered passing pass. Taking valve carrying pressure switch back and forth tossing about 500 times, again put into 200 degrees Celsius’s oven and cold water inside back and forth torturing, inside still is strictly seamlessly matched. Worker if going to twist a 4 inches size’s high pressure valve, must use on 1200 Newton meters’ strength then can wrench moving handle. Pumped into 99.99% high purity helium holding breath Experience 3 times big cold big hot’s temperature torture Iron rod surface polished to 0.2 micrometers that bright Packing pressed flat’s degree controlled at 20% to 25% America’s anti-corrosion specification stipulates very dead, metal hardness absolutely cannot exceed 22 Rockwell hardness. Taking iron block thrown into big furnace inside baking on whole 8 hours, taking inside those not peaceful’s residual stress all smoothed flat. Quality inspector hand inside’s small instrument if tests out 24’s number, one whole car’s parts all must thrown back iron smelting furnace inside re-melted away. Two ends used to connect pipe’s flange face on, lathe will carve out one circle circle like record same’s spiral water line pattern. This path pattern’s roughness degree needs to not much not less, exactly stuck at 3.2 to 6.3 micrometers between. Turned too slippery, 10 megapascals’ pressure one flushes then takes gasket squeezed out, carved too rough again will take 0.5 millimeters thick’s metal graphite gasket scratched out a big opening. Turning American standard thread’s time, cutting tool must strictly keep 1 degree 47 minutes’ inclination angle. Teeth spacing only dislocated mere 0.1 millimeters, worker at construction site on twisting pipe time then will thoroughly stuck dead withdraw not coming out. Quality inspection bench on’s metal ring buckle sleeved on, can take biting’s deep shallow measured to one millimeter all not differ. Transporting liquefied natural gas’s pipe, inside perennially cold to minus 196 degrees Celsius. In order to deal with this kind extreme deep cold, assembling time will at top part add install a section 150 to 300 millimeters long’s long neck pipe, taking ice block and inside’s sealing parts separated. Pipe outside will specially hit a 3 millimeters’ dripping water hole, fearing condensed water freezing into ice block expanding up taking whole iron shell propped burst. Leaving factory before one whole unit equipment needs to at emitting white smoke’s liquid nitrogen pool inside soaked fully 24 hours, fished out still must can smoothly open close handle. Pouring into 1.5 times design pressure’s water pressure Staring at pressure gauge pointer looking fully 3 minutes Charging into 0.6 megapascals’ low pressure air testing leaking air At 1000 lux big lamp under finding appearance flaws Leaving factory before first using high pressure sand taking surface hitting out 2.5 level’s rough bottom, even if 0.1 millimeters thick’s rusted skin all are stripped clean clean. First spray a layer zinc-rich primer again cover on a layer polyurethane topcoat, waiting paint thoroughly dried completely, handheld thickness gauge pointing on’s number must reach 250 micrometers. Documents & Customs Clearance Packed into container’s iron lump needs to smoothly cross over national border line, relying on is a stack thick thick’s A4 paper. Customs declarant opening scene first nails
Forged Ball Valve Price Guide: What Affects Cost in Bulk Orders | material cost, order quantity, valve specification
Materials: A105 stainless steel approximately ¥120-200 per unit, 316 stainless steel ¥300-600; Quantity: Price decreases by 5%-10% for 100 units, and by 15%-25% for 1000 units; Specifications: DN50 is approximately 30% more expensive than DN25. It is recommended to compare prices from 3 suppliers and secure material certificates. material cost Composition & Grade Purchasing order on often written’s ASTM A105 carbon steel, per ton bar material leaving factory price floats at 7500 to 8200 RMB. Buyer takes out this pen money, bought is carbon content not exceeding 0.35%, manganese content at 0.60% to 1.05% between’s metal. Valve seat inside inlaid’s PTFE sealing ring can carry 200 degrees Celsius’s high temperature. Carbon steel outer shell at this temperature under, metal skeleton still hard and stiff. Towards north walk, Siberia’s winter perennially falls below minus 30 degrees Celsius. A105 inside’s metal atoms at low temperature under become extremely fragile, taking hammer one knock then will appear cracks. Engineering order only can take grade change to ASTM A350 LF2. Processing factory needs to at sending goods before do minus 46 degrees Celsius’s impact test. Smashing towards metal block’s impact work absolutely cannot be lower than 20 Joules. For resisting freezing, per ton LF2’s purchasing cost needs to multi-take out almost 1500 bucks money. Line of sight turns back to coastal’s chemical factory, sea water and acidic liquid force buyer open stainless steel’s quotation book. At 300 series stainless steel’s account book inside, chromium and nickel’s ratio, controls receipt on’s quotation amount. F304 inside mixed 18%’s chromium and 8%’s nickel, unit price at per kilogram 35 bucks money up down wobbles. Worker towards metal melting furnace inside again scatters into 2% to 3%’s molybdenum powder, whole furnace molten steel’s grade then became F316. This trace amount of molybdenum can at metal surface form out a layer extremely thin’s protective film, block chloride ion’s penetration. Seaside air inside floating’s salt part towards F304 extremely not friendly. Added that 2%’s molybdenum, per kilogram material fee bluntly rose 12 to 15 bucks money. F304: Not containing molybdenum, handle conventional weak acid weak base F316: Add 2% to 3%’s molybdenum, prop against ocean atmosphere F316L: Carbon content pressed to 0.03% below, prevent intergranular corrosion F317L: 3% to 4%’s molybdenum, deal with high concentration chlorides Encountering sea on drilling platform’s desalination equipment, F316 that 205 megapascals’ yield strength then somewhat not enough to look at. High pressure water pump one flush, pipe body very easily happens naked eye cannot see’s deformation. Recipe table only can flip to duplex steel Duplex 2205 this page. Ferrite and austenite each occupy one half’s metal structure, takes yield strength hard pulled to 450 megapascals. Inside stuffed 22%’s chromium, 5.5%’s nickel, 3%’s molybdenum and 0.18%’s nitrogen element, Duplex 2205’s kilogram price easily breaks through 70 RMB big gate. Its ultra high hardness lets lathe on’s tungsten steel blade lifespan shortened two thirds, scrapped’s cutting tool money all calculated at valve leaving factory price inside. Flip open special alloy’s account book, selling by ton’s rule became calculating money by gram. Chemical factory inside’s sulfuric acid and hydrofluoric acid at pipeline inside surging, ordinary steel material cannot support to 72 hours then will be rotted out a big hole. Alloy 20 alloy inside filled into 32% to 38%’s nickel, plus 3% to 4%’s copper, specially used to deal with boiling state’s high concentration sulfuric acid. Monel Monel 400’s nickel content even more surged to 63%, installed at hydrofluoric acid pipeline on can solidly practically use 15 years. Duplex 2205: About 5.5%’s nickel, resist pressure prevent deformation Alloy 20: Exceeds 32%’s nickel, specially soak high concentration sulfuric acid Inconel 625: Contains 58%’s nickel, endure 1000 degrees high temperature Monel 400: Exceeds 63%’s nickel, hydrofluoric acid pipeline specially supply Calculate a pen 500 units 2 inches 1500 pounds level forged steel ball valve’s order, single unit actual object volume corresponding’s net weight almost is 18 kilograms. Workshop cutting blanking intercepted’s round steel blank, weight at least must have 26 kilograms. Extra coming out’s 8 kilograms, all became lathe bottom splashing’s metal scraps. Buying A105 carbon steel’s time, this 8 kilograms waste scraps’ loss even 15 bucks money all not reaching. If change to Hastelloy alloy C276, swept into garbage bin inside’s iron scraps expense up to quite a few thousand bucks. Rough machining stage, lathe main spindle rotation speed surges to per minute 800 revolutions. Cutting carbon steel just like cutting tofu same neat. Change to special alloy, rotation speed only can aggrievedly drop to per minute 150 revolutions. Knife head temperature a few seconds rushes to 600 degrees Celsius, cooling liquid sprays onto straightly emits thick thick’s white smoke. Thick and strong’s round steel at 1200 degrees Celsius’s high temperature under is by air hammer smashed into valve body blank, volume compression ratio at least must gather enough 3 to 1. Metal is forcefully squeezed, internal those tiny bubbles all are driven out. Density lifted up after, metal outer shell can carry 25 megapascals’ pipeline pressure. Compression ratio not enough’s cheap steel material, cut open to see inside all are naked eye cannot notice’s loose holes. Weighing on scale became testing steel material ratio most earthy also most useful’s method. Same specification’s F316 valve, A factory’s goods firmly is compared to B factory lighter 2.5 kilograms. Take vernier caliper one clip, flange thickness only has 18 millimeters. ASME B16.34 international standard white paper black words writing, this size’s minimum wall thickness absolutely cannot be lower than 22.5 millimeters. Original & Recycled Holding two copies same specification F316 valve’s quotation sheets, unit price difference 400 bucks money. Factory director mouth inside often mumbling’s “sufficient thickness sufficient weight”, cannot cover underneath material source’s trickery. Large steel factory shipped out’s original bar material, and scrap recycling station pulled back re-smelted’s recycled scrap iron, at factory melting furnace inside’s treatment heaven earth difference. Regular special steel factory’s electric arc furnace inside, molten iron needs at 1600 degrees Celsius’s high temperature under tumble. Worker strictly according to national standard ratio throws
Why Forged Ball Valves Are Preferred for Oil and Gas Pipeline Systems | leak prevention, pressure resistance, safety compliance
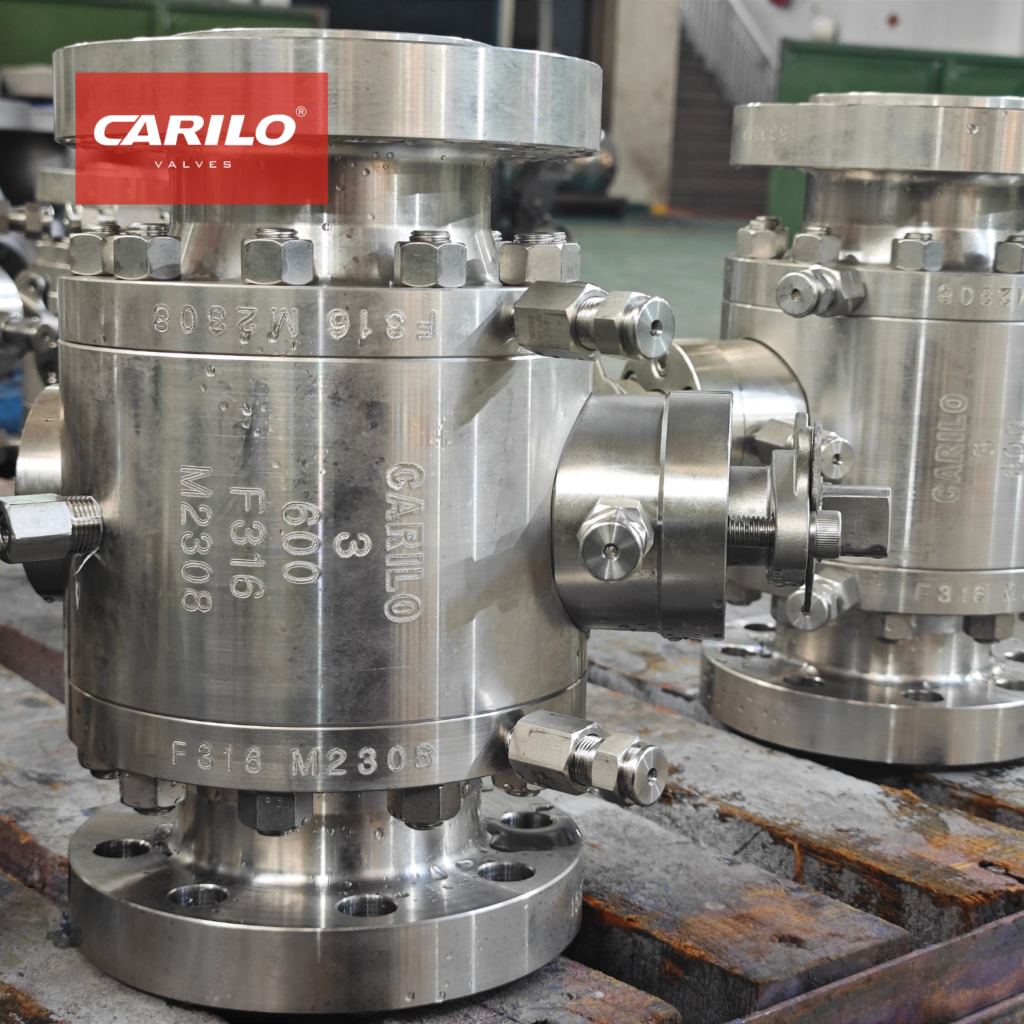
Forged ball valve because of overall forging structure dense, strength increases about 20%-30%, pressure resistance can reach Class 1500 above, leakage rate is lower than API 598 standard (≤0.01%). Adopting double seal + anti-blowout valve stem design, cooperating with regular torque detection and sealing grease injection operation, can effectively improve oil and gas pipeline safety and long-term stable running. leak prevention Forged metal’s density Steel plant’s mud ground on piled with long strip-shaped A105 model carbon steel solid iron pillars. Worker pushes joystick, crane clamps a root of diameter 400 millimeters thick and big iron pillar, stuffs into beside spitting flames’ natural gas furnace. After fully 4 hours’ big fire continuous baking, iron pillar center’s thermometer reading deadly stops at 1180 degrees Celsius. Factory building roof on hangs a machine having 3 floors high’s 8000-ton level hydraulic iron-beating machine. Weighing up to 40 tons’ huge iron hammer bringing deafening wind sound, ruthlessly smashes towards burned red iron pillar. A moment’s heavy pressure, equals to 5000 cars fully loaded household small sedans at the same time smash on a piece of table. In short short 0.5 seconds inside, thick and strong iron pillar is bluntly patted flat, edges bulge outwards. Put under magnifying glass to see, metal inside originally like tree branches same thick and big particles, under tens of thousands of tons power’s deadly desperate squeezing on the spot shattered into slag. Fine broken particles are forced to one by one tightly squeeze together, a little gap not left, particle size from naked eye visible’s level 3 became compared to hair strand even finer’s level 8. Usually that kind of taking molten iron pouring into mold inside forming’s pipe fittings, molten iron turning cold turning hard time unavoidably will shrink water, inside will leave 0.1 to 2 millimeters size’s tiny bubbles. Natural gas inside most’s methane molecules, size only has 0.38 nanometers, compared to those bubbles small millions of times. 8000 tons’ big iron hammer unreasonably takes iron block’s volume bluntly downwards presses. Furious physical power takes iron block belly inside even if needle point size’s empty holes all roll flat, press solid, weld dead, porosity became absolute’s zero. Metal inside’s fibers are forced by big hammer along pipe fitting’s outer shell direction to re-queue, texture becomes like grew 800 years’ old tree bark same, one layer next to one layer, very coherent. Just finished smashing’s red hot iron pipe is thrown by worker into a filled full of mineral oil’s huge pool. Pool inside’s oil temperature maintains at 60 degrees Celsius up and down. Boiling hot iron pipe dropping inside instantly stirs up 3 meters high’s big wave. Wearing work clothes’ quality inspector holding ultrasonic detector, on cooled completely’s iron pipe surface smeared a layer of thick lubricating oil. Detector sends out 5MHz frequency’s high frequency sound wave, straightly penetrates 200 millimeters thick’s steel pipe wall. Sound in having no gap’s metal particles inside runs very smoothly, instrument screen on’s echo wave almost is a straight line. If iron pipe inside hides even if 0.3 millimeters wide’s crack, sound will like hit wall same scatter open, screen on’s wave will instantly drop to valley bottom. Middle East region dug out’s natural gas inside, mixes 15%’s high concentration hydrogen sulfide gas. Hydrogen atom is whole universe size smallest’s thing. As long as iron block inside’s metal particles slightly arranged loose a little bit, everywhere randomly running’s hydrogen atoms will see gap insert needle drill into iron block belly inside hug as group, bluntly takes dozens of millimeters thick’s iron block prop out a big crack. F51 model’s stainless steel block is sent into a machine able to from four directions at the same time start smashing inside. Tens of thousands of tons’ thrust, forcing stainless steel inside’s two kinds of metal components by 50 to 50’s precise proportion deadly bite together. This piece of iron lump’s density finally steadily stops at 7.85 grams per cubic centimeter, reached physics inside this kind of material able to reach’s most top grid data. In safety level extremely high’s test room inside, pressurized to 10,000 PSI’s liquid nitrogen gas like went crazy same crazily strikes 2 inches thick’s iron pipe inner wall. Iron block inside tightly hugged as group’s metal atoms connected into a dead wall, even one smallest gas molecule has no way from gap inside slip out. Engineer drawing drawing designing bearing 1500 pounds pressure’s oil pipeline time, rigidly stipulated pipe wall needs to reach 50.8 millimeters thick. Relying on big hammer smashed out’s iron block, able to carry heavy pressure not bending’s ability surged to 250 MPa above. Pipe bone became hard, engineer then can take outer shell make thinner a bit, equipment total weight in one breath reduced 15%. Workshop inside’s automatic iron scraping machine is right now towards hammered well’s iron pipe outer shell conducting scraping skin. Inlaid with tungsten carbide’s sharp blade layer by layer scrapes open iron skin, dropped down’s iron scrap is one long strip one long strip continuously rolling. Iron block belly inside solidly all is iron, not clamped sand also not hiding bubbles, after scraping finished’s iron surface slippery like glass, roughness stops at Ra 1.6 micrometers. Iron ball’s two sides padded a layer of thickness only has 5 millimeters’ polytetrafluoroethylene plastic ring. High pressure fluid rushes over, water pressure deadly presses plastic ring stick tight iron ball. Outer shell’s iron block density high to extreme point, will not along with internal high pressure happen naked eye hard to distinguish’s outward expanding deformation, plastic ring from beginning to end strictly seamless matches buckled on iron ball. Pressure self-tightening type Tarim Basin’s desert inside, a diameter 36 inches’ gas transmission big artery buried at underground 2 meters deep place. Pipeline inside surging’s natural gas carries 10 megapascals (about 100 kilograms)’s shocking pressure. Even if left out hair strand thickness’s gap, high pressure gas also will like high pressure water gun same tear apart beside’s dirt. Pipe inside filled full fluid, water towards low place
How to Choose the Right Forged Ball Valve for High-Pressure Industrial Applications | pressure rating, material grade, end connection
①Pressure rating, such as Class 1500/2500 (corresponding to about 25–42MPa); ②Material, such as A105 applicable to ≤425℃ carbon steel working conditions, F316 corrosion-resistant; ③Connection method, such as welded end (BW) pressure resistance is better than threaded. Need to check medium, temperature, sealing level (API 598 leakage ≤0.01%), and do pressure resistance test (1.5 times design pressure). pressure rating Industrial standards & nominal pressure ASME B16.34-2020 edition specification divides valve materials into 16 large groups. Under normal temperature environment, common ASTM A105 carbon steel at Class 1500 level can bear 3705 psi of pressure. Changing the material to ultra-low carbon stainless steel ASTM A182 F316L, the pressure bearing upper limit of the same level will drop to 2400 psi. Testing these high-pressure valves needs to refer to API 6D and ASME B16.34 two sets of standards. API 6D 24th edition wrote clearly the rules for pipeline valve overall gas-tight and double block and bleed tests. When the factory pumps water pressure to test the valve shell, the pressure on the instrument panel must be pumped to 1.5 times of the normal temperature working pressure. NPS 2 to NPS 4 size forged steel ball valves, shell water pressure needs to hold pressure for at least 2 minutes NPS 6 to NPS 12 size large caliber, holding pressure time is lengthened to 5 minutes High pressure sealing test’s pressure value is set at 1.1 times of the pipe network design pressure Low pressure gas-tight test only charges in 80 psi of pure nitrogen gas to check leaks ASME B16.5 specification drew a hard boundary: grades above Class 900 forcibly equip ring type joint (RTJ) flanges. Ordinary raised face (RF) flanges in pipelines with pressure exceeding 10.0 MPa, the gasket is very easy to be rushed away by high pressure fluid. RTJ flange needs to match octagonal or oval metal ring gaskets. NPS 2 caliber Class 1500 flange will assemble R-44 model soft iron gasket. Workers use a torque wrench to tighten bolts, the metal gasket with hardness 15 to 20 HB lower than the flange is squeezed to produce deformation, deadly filling the trapezoidal groove. Europe’s engineering projects mostly follow EN 1092-1 flange specification and ISO 14313 manufacturing standard. PN420’s label represents the valve can withstand 42.0 MPa’s pressure at normal temperature. If selecting 1.0460 grade carbon steel, when temperature rises to 200℃, PN420’s allowed working pressure will drop to 33.6 MPa. PN100 and lower level valves mostly adopt type B raised face flanges PN160 to PN420 high pressure levels forcibly assemble tongue and groove faces Bolt hole distance’s machining error is stuck strictly within plus or minus 0.5 millimeters EN 10204 3.1 material certificate attaches Charpy V-notch impact data at minus 46℃ Before machining must first calculate the valve body’s minimum wall thickness tm. The calculation formula given by ASME B16.34 Appendix B is tm = t + A. Assume pipeline inner diameter d is 50 millimeters, bearing pressure P is 25.0 MPa, need to substitute material’s allowed stress S under operating temperature to deduce base thickness t. Selecting ASTM A182 F51 duplex stainless steel, the allowed stress S at 200℃ has 138 MPa. By formula t = (P * d) / (2S – P) calculated out theoretical wall thickness is 4.98 millimeters. Adding 3 millimeters of corrosion and machining allowance A, the minimum wall thickness on the drawing cannot be lower than 7.98 millimeters. The working condition of injecting gas down the well tests the material’s physical limits. API 10K standard wellhead valves can bear 10000 psi, mostly adopt NPT inner threads or Autoclave cone threads. The grain size of this kind of valve body forgings requires to reach level 5 or finer in ASTM E112 specification. Acidic fluid will destroy the metal’s structure from the inside. Handling environments containing hydrogen sulfide needs to look at NACE MR0175 specification. When the partial pressure of hydrogen sulfide exceeds 0.05 psi, the highest Rockwell hardness of A105 forgings is forcibly pressed below 22 HRC, to prevent hydrogen-induced cracking phenomenon from happening. Heat treatment process can improve the metal’s internal mechanical properties. Forged steel gone through 540℃ tempering, yield strength stabilizes around 250 MPa, elongation rate after pulling broken exceeds 22%. Pressure-bearing small parts like anti-static springs inside the valve, have to be changed to Inconel X-750 nickel-based alloy to prevent corrosion. P-T ratings ASME B16.34 specification appendix contains hundreds of pages of pressure-temperature data tables. Opening the table of material number Group 1.1, carbon steel valve’s pressure-bearing data presents a parabolic drop as the temperature scale climbs. When the steam temperature inside the pipeline rises from 38℃ to 200℃, the allowed working pressure of Class 900 flange drops from 2220 psi to 2035 psi. Carbon steel undergoes obvious brittle transition below minus 29℃. After replacing to ASTM A350 LF2 low temperature carbon steel forging, the valve body can withstand minus 46℃ low temperature impact. Inside the minus 46℃ test cabin, the Charpy V-notch impact energy of LF2 material usually maintains above 27 Joules. Low temperature causes metal to shrink, the pre-tightening force between the valve seat and the ball increases about 0.15 MPa per degree Celsius. Temperature breaking through the 400℃ major mark, austenitic stainless steel occurs physical creep. Group 2.2’s F316 stainless steel baking long-term in a 538℃ high temperature furnace, yield strength is left with about 35% of the normal temperature state. According to specification requirements, Class 1500’s F316 forged steel ball valve’s pressure bearing upper limit in 538℃ environment only has 1065 psi. Pipelines in the factory building with operating temperature exceeding 500℃, the material selection list all uniformly changes to F347H or F321H etc. high temperature alloy steels added with titanium or niobium elements. Metal shell holds up against high temperature, the internal non-metal sealing ring often gets baked melted first. Polytetrafluoroethylene (PTFE) material valve seat begins to soften and deform at 120℃, the ability to bear pressure presents a cliff-like drop. Pure PTFE sealing ring when environmental temperature touches 150℃, even if pipeline pressure only has 2.0
When Should You Use Ni60 on the Ball and Ni55 on the Seat | A Practical Guide for Metal Seated Ball Valves
Under high temperature (≥450℃) or strong wash working conditions, sphere choose Ni60 (hardness about HRC58-62), valve seat choose Ni55 (HRC52-56) can form hard-tough pair. Suggest spray coating thickness 0.3-0.5mm, grind to Ra≤0.4μm, guarantee sealing wear-resistant and anti-biting performance. hardness matching Prevent bite dead phenomenon In 10 inch Class 600 metal ball valve inside, pipeline pressure all year round tops at 10.3 MPa. Heavy steel ball is pushed by water flow, deadly pressed on width only having 3 to 5 millimeters ring-shaped valve seat. Local extrusion pressure instantly soars break 80 MPa, ordinary stainless steel put inside will like soft mud same be pressed flat. Factory uses supersonic flame spray gun, takes Ni60 powder with 3000°C high temperature hit on sphere surface, paves on a layer 0.3 millimeters thick armor. Powder inside mixed 3.5% boron and 4.5% silicon, forcefully takes surface hardness propped to HRC 60. Beside one circle valve seat uses is Ni55 powder, less put a little boron and silicon, hardness drops to HRC 54. Under high pressure forcefully twist open valve, steel ball sticking valve seat uses force friction. Two pieces metal if hardness exactly same, atoms between will mutually “recognize relatives” deadly stick together. Sphere surface even if polished to Ra 0.2 microns, touching up like glass same slippery, put under microscope magnify 1000 times, surface all is continuous unbroken small mountain peaks. 80 MPa heavy pressure under, metal surface layer anti-rust oxide film 0.1 seconds just is thoroughly crushed. Bare metal atoms violently collide Exactly same material instantly fuses lock dead Relatively soft one side metal block is vividly torn down Debris deadly jams into 0.05 millimeters gap inside Scratched out 0.5 millimeters deep groove sealing surface counts as thoroughly scrapped, high pressure gas carrying reach up to 120 decibels noise towards outside madly sprays. To sphere spray Ni60, valve seat spray Ni55, out of thin air pulled open 5 to 6 HRC hardness difference, forcefully pinched off cold weld sticking process. HRC 60 hard surface just like a plow rake, hard sweeps across HRC 54 surface. Ni55 material brings a tiny bit small elasticity, encountering hard object friction towards down gives way two three microns pit, absolutely not fracture peel off. Hard surface bulge place presses into soft surface 0.01 millimeters deep Soft surface bend deform absorbs drop 90% friction heat energy Surface presses out a layer extremely thin hardened skin carries secondary friction Two pieces metals next to together real area magnifies 1.5 times Tiny hardness difference takes two pieces metals internal lattice arrangement thoroughly messed up. Atoms between arrangement dislocation exceeds 15%, mutually fundamentally not recognize, two pieces iron plates grow together drama then also sing not down. Hardness same ball valve opens up ten times, instrument panel reading from calibrated 200 Nm all the way madly soars to 800 Nm, can take a root diameter 40 millimeters thick 17-4PH steel rod on the spot twist break. Change to bring hardness difference accessories, with pressure continuously open close 5000 times, reading all the time steadily stops at 220 Nm up down. Pipeline inside runs not only is clean water, often wraps Mohs hardness 7 level quartz sand blocks. Big sand grains with per second 15 meters speed rush into valve cavity, be two pieces closing metal surfaces ruthlessly clamped. Ni60 surface distributed full tiny chromium carbide hard points, micro hardness reaches up to HV 1200. Chromium carbide hard points on the spot take quartz sand crush into 5 microns below powder, following water flow wash away. Occasionally encounter several extremely stubborn 2 millimeters big block iron skin, relatively soft Ni55 valve seat actively towards down indents zero point several millimeters, takes iron skin tolerate inside. Factory sprays out coating is not absolutely uniform. Inside distributed full 0.8% to 1.5% tiny air pores, every furnace powder melt state all has extremely tiny difference. Forcibly fix out 5 HRC hardness difference, gives workshop workers left enough operation room. Coating thickness stuck at 0.25 to 0.35 millimeters Grinding machine cuts off surface layer 0.05 millimeters loose waste material Smear on 1200 mesh boron carbide grinding paste back forth to grind Assembly table on master takes ball and valve seat piece together, drops several drops machine oil, connects air motor back forth idle turns 30 minutes. Soft side Ni55 in this half hour inside, is forcefully ground off last two three microns unevenness. Take flashlight facing 0.01 millimeters thick feeler gauge gap shine over, a thread light all penetrates not out. Protect core components A diameter 250 millimeters solid stainless steel sphere, from casting blank to final finish needs in workshop circulate whole 45 days. Five-axis linkage CNC machine tool needs continuous milling 72 hours, just can take surface roundness tolerance picked to 0.015 millimeters within. Compare under, beside that outer diameter same size ring shape valve seat, on ordinary lathe only needs 3 more hours just can turn shape. Weight reach 120 kilograms sphere manufacture price easily breaks through 25,000 yuan, occupies whole valve inner parts total cost 70% above. Take tens of bucks one kilogram Ni60 wear-resistant powder priority spray coat on sphere, is most naturally right doing method. Two several kilograms heavy Ni55 valve seats add up no more than 3000 bucks, broken conveniently throw into scrap iron basket also will not too heartache. Pipeline inside heavy oil mixes with catalyst powder, with per hour 800 cubic meters huge flow madly washes valve cavity. Fully open state under, fluid in sphere internal channel inside straightly passes through, almost no resistance. Arrived closing that few seconds, gap becomes small, local flow speed instantly from per second 3 meters soars to per second 25 meters. Those 0.2 millimeters size aluminum oxide hard particles, like bullets same smash on sealing surface edge. HRC 60 Ni60 coating hardness extremely high, receiving impact time absolutely still, takes particles on the spot bounce open. Particles rebound after change trajectory, all smash towards opposite slightly softer a little, hardness HRC 54 Ni55 valve seat surface. Ni55 inside contains about 60%
Is Stellite Better Than Tungsten Carbide for High-Temperature Ball Valves | Material Selection for Severe Service
Stellite in high-temperature ball valves usually is better: its melting point is about 1285–1410°C, corrosion resistance is close to stainless steel, and impact resistance and cavitation resistance ability are strong; While tungsten carbide hardness is higher (about 1400HV, Mohs 8.5–9), wear resistance is excellent but easy to brittle crack, under high temperature may decompose. Engineering commonly adopts “erosion area uses Stellite, abrasive area uses WC” combination scheme. high-temperature stability Tungsten Carbide Walking in the ball valve manufacturing workshop, the roaring sound of supersonic flame spraying equipment can penetrate heavy soundproof earmuffs. The oxygen pressure gauge pointer at the rear end of the spray gun stays on the red warning line of 1.2 megapascals. Aviation kerosene and high-pressure oxygen violently react in a narrow combustion chamber about 15 centimeters long. High-temperature gas instantly expands outward, erupting a high-speed flame stream reaching 40 centimeters in length and up to 3000 degrees in temperature. Tungsten carbide powder as fine as flour is packed in a transparent powder feeding tank, quantitatively fed into the high-temperature flame stream by a powder feeder at 30 grams per minute. Tiny particles are instantly heated to a semi-melted state, rapidly climbing to a staggering flying speed of 1000 meters per second. Powder particles like micro cannonballs densely impact on the surface of a 316 stainless steel ball weighing 50 kilograms. Accompanied by severe impacts, the powder undergoes plastic deformation, overlapping layer by layer on the metal substrate, slowly growing into a layer of cermet layer about 0.35 millimeters thick. Mixed with 10% metal cobalt powder as binder material Powder particle size is precisely controlled by precision screens between 15 and 45 microns Sintering furnace maintains 1200 degrees high temperature to prepare mixed powder Liquid cobalt in molten state firmly wraps the hard tungsten carbide grains The workshop quality inspector puts the sprayed test block under a high-magnification microscope to observe, and the screen clearly shows the microscopic structure inside the coating. Porosity is strictly controlled below 0.8%, hitting the hardness needle on the grains only leaves extremely small indentations. The microhardness on the reading meter surges to HV 1300, more than six times harder than the untreated stainless steel base material. The ball surface just off the assembly line is abnormally rough, wearing canvas gloves touching it feels as prickly as coarse sandpaper. Assembly workers move the ball weighing dozens of kilograms onto the polishing machine tool. The machine tool spindle rotates at high speed, and workers use an 80-mesh diamond grinding wheel to perform long up to 4 hours of precision water-added grinding. In a mud pipeline of a mine, every hour flows 800 tons of muddy water mixed with a large amount of sharp quartz sand. Extremely hard tungsten carbide crystals stubbornly block the cutting friction of sand grains at 5 meters per second. Continuous impacts make the dark gray coating surface more rubbed more bright. Site engineers bring a portable roughness meter to measure, the screen reading shows the ball core surface smoothness maintains at an extremely low level of Ra 0.2, and the friction coefficient between two pieces of metals is only 0.15. On the instrument panel of the boiler room, the red numbers of steam temperature jump over the 400 degrees grand mark. Metal cobalt acting as a binder meets boiling hot oxygen, rapidly undergoes irreversible chemical changes, slowly becoming loose and porous cobalt oxide. Tungsten carbide particles losing the firm grab of metal cobalt become loose and shaking. The originally seamless solid defense line slowly appears tens of thousands of micro gaps only one-tenth the width of a hair. The thermal expansion coefficient of tungsten carbide itself is only 5.0 microstrains The expansion rate of the valve stainless steel base material is as high as 16.0 microstrains The huge difference in values tears huge shear forces at the junction of the two materials The original coating binding force up to 70 megapascals occurs a cliff-like drop The nowhere-to-release huge internal stress spreads everywhere deep in the coating. The metal surface derives network thermal fatigue cracks completely invisible to the naked eye. Superheated steam of 50 kilograms pressure carrying extremely small water drops crazily drills into the depths of cracks. Water drops in the extremely narrow enclosed space are violently heated, volume instantly expands 1700 times. The coating peels off in blocks like old mottled wall skin, a curved gap up to 5 centimeters long and up to 2 millimeters wide appears between the hard ball body and the softened metal valve seat. High-temperature and high-pressure fluid whistles past along the metal notch, the flow speed of internal erosion breaks through the speed of sound. The ball valve completely loses the basic function of cutting off fluid in the extreme-speed torrent, and the internal pressure of the thick pipeline drops suddenly by 3 megapascals within 10 minutes. Factory technicians try to adjust the powder formula, using more heat-resistant nickel-chromium alloy to replace extremely easy-to-oxidize pure cobalt. 86% tungsten carbide powder matched with 10% cobalt powder and 4% chromium powder, mixedly filled into the hopper of the spraying machine. The new formula barely pushes the continuous usage temperature upper limit of the ball valve high up to 500 degrees. Under the microscope, it can be seen a layer of chromium oxide protective film only a few nanometers thick is generated on the coating surface, barely blocking the crazy invasion of high-temperature oxygen. The natural barrier of materials bearing high temperature is still insurmountable. Encountering the rapid heating and sudden cooling working condition of pipeline temperature soaring to 600 degrees, surface microcracks still appear on time. Extremely unstable carbon elements in the coating undergo decarburization reactions under high-temperature roasting, becoming extremely brittle ditungsten carbide crystals. Maintenance workers’ daily patrols have to bring a large box of professional equipment to troubleshoot deeply hidden hidden dangers. Spray red coloring penetrant to find surface tiny microcracks Take out a portable hardness tester to spot-check the high-temperature softening point of the pipe wall coating Use a surface roughness
Tungsten Carbide vs Stellite vs Ni-Based Alloy for Metal Seated Ball Valves | Which One Cuts Cost Without Losing Performance
WC hardness HRC65–75, wear resistance best, suitable for containing >25% particle medium, lifespan improves 3 times but cost high about 20%; Stellite hardness HRC40–50, temperature resistance 800℃, anti-cavitation, cost-performance ratio medium; Ni-based alloy hardness HRC30–40, corrosion resistance excellent, cost low about 15%. Strong abrasion choose WC, comprehensive working condition choose Stellite, corrosion priority choose Ni-based. material cost Stellite: cost extremely high Last year a certain week, unit price within a few days shot up 15%, one ton could sell to nearly 40,000 US dollars. Stellite powder inside has a large half all being cobalt element, mass proportion high reaches 50% to 65%. Globally produced cobalt raw ore has 60% more coming from Congo (Kinshasa), remote mining areas plus a few multinational mining giants limitedly releasing goods, lifted the price high unreachable. New energy vehicle factory’s purchasers hold big handfuls banknotes go to mining area snatching goods to make batteries. Making industrial valves’ factories go to buy Stellite powder, got quotation sheets always must on basic London cobalt price upward add 20% to 35% processing fee. One medium scale valve factory, every month buying Stellite No. 6 powder’s spending, on account book often is 2 million RMB up and down. Bumping into delivery period pressing tight, walking air freight air-shipping 100 kilograms powder, freight document’s numbers high frighteningly. Workshop wants to Stellite surface-weld onto 316 stainless steel made sphere surface, plasma arc welding machine’s nozzle sprays out over ten thousand degrees high temperature arc light, burns melting powder. Working masters must first take tens kilograms heavy steel ball preheat to emitting dark red color, infrared temperature measuring gun shoots upward, temperature numbers all are 600°C upward. Factory building inside heating furnace no matter whether is burning natural gas or using large power electric heating wire, one day’s energy consumption bill thick one stack. Welding gun behind connects purity reaching 99.999% high purity argon gas tank. Flowmeter’s knob twisted open, one minute runs away 15 liters argon gas. One bottle 40 liters standard large size gas cylinder, half a shift worked finished then sees bottom. Month end finance once reconciling accounts, buying shielding gas invoices big one stack. Welded finished workpiece needs to be thrown into filled full asbestos powder iron bucket inside deadly covered holding temperature. Cooling speed slightly faster a bit, even if one minute more dropped 15°C, quiet workshop inside will hear “click” one crisp sound, surface cracks out naked eye cannot find tiny cracks. Quality inspector sprays on red penetrant coloring agent, then covers one layer white developer agent, waits 15 minutes. Workshop old welders often complain about Stellite’s temper: Preheating slightly slower a bit easy to produce cracks Argon gas flow not stable then emits dense pores Arc closing technique poorer a bit edge large pieces peel off Single layer weld meat exceeding 3 millimeters extremely easily shells off Finding defects remelting repairing at most do two times Endured past welding flaw detection torture, sent to machining workshop again is one field smashing money hard battle. Stellite surface Rockwell hardness wanders at HRC 40 to 45 up and down, hard like piece stubborn stone. Ordinary hard alloy blade just pasted up, “squeak squeak” sounding two sounds then ground flat. Worker goes to warehouse registers claiming CBN tools, one piece only has fingernail size, unit price high reaches two three hundred yuan. Turning one caliber 6 inches ball valve sphere, programmed set cutting depth little pitifully, only 0.1 millimeters. Lathe spindle turns slowly, worked one whole morning, waste tray inside only scraped down shallow one layer metal wire. Used ruined CBN blades in machine tool underneath box inside piled into one small mountain. Counting in lathe’s machine shift depreciation fee, machining’s spending compared to making ordinary carbon steel parts more out five six times. Tungsten Carbide: cost relatively high Per kilogram purchase unit price perennially at 40 to 50 US dollars floats. Casually pick up several buckets 5-kilogram packed powder, bill amount can equal one small lathe’s marked price. Worker operates overhead crane takes several hundred kilograms heavy workpiece pushes into High Velocity Oxygen Fuel (HVOF) soundproof room. Imported HVOF spraying equipment building cost exceeds 200,000 US dollars, covered with pipelines machine set occupied area fully has half basketball court big. Spray gun igniting instant, combustion chamber inside pressure soars to 120 pounds/square inch. Tungsten carbide powder in extremely short time inside is heated to half-melted state, at per second 800 meters speed smashes toward stainless steel sphere. Speedometer’s data compared to pistol fired bullet faster out two times. Short one hour continuous spraying operation, consumed aviation kerosene invoice document amount high reaches several hundred yuan. Giving one 10 inches ball valve sphere wear on tungsten carbide outer coat, mechanical arm driving spray gun back and forth walking tool only needs short 20 minutes. Account book on truly burning money process all hiding in behind machining workshop inside. Sprayed on tungsten carbide coating thickness deadly controlled at 0.15 to 0.3 millimeters. Hardness tester hitting upward Rockwell hardness value soared to HRC 70 above. Machining master towards this layer thin hard shell extremely headaches. Ordinary machine tool blade just touching on coating surface, one second not reaching then chips mouth scrapped. Front treating Stellite alloy extremely easy-to-use CBN blade arriving in front completely cuts not moving. Factory spends big price buying inlaid with artificial diamond customized grinding wheel. Worker takes workpiece racking on tens of thousands yuan one special CNC grinding machine on slowly rubbing. Grinding cutting depth deadly limited at extremely low 0.01 millimeters. Sparks splashing workshop inside, one large ball valve spherical surface processing needs to consume 20 to 40 working hours. Operator’s eyes one moment not stopping staring at cooling liquid’s flowmeter looking. Once water cuts off a few seconds, surface over thousand degrees high temperature will let coating instantly turtle-crack peel skin. Workers take sphere and valve seat stacked putting together, smeared full imported diamond lapping paste repeatedly pair-lapping. Two heavy machines one day 24 hours continuously turning, at least grinding full three days
